Best Ring Joint Gaskets Supplier for Reliable Industrial Sealing
2026-10-10
A flange leak at 10,000 psi doesn't just ruin a shift—it can trigger a shutdown that costs more than a year's supply of gaskets. That's why ring joint gaskets aren't a place to cut corners. Kaxite has built its name on precisely machined metal gaskets that maintain seal integrity in the harshest oil and gas, petrochemical, and power generation environments. Instead of promising miracles, Kaxite focuses on the details that actually matter: controlled hardness, proper surface finish, and full material traceability. This article unpacks what makes a ring joint gasket reliable—and what to demand from your supplier before the next pressure cycle.
Material Choices That Outlast Harsh Industrial Cycles
Selecting the right materials for industrial environments means looking beyond initial cost and considering how they hold up under repeated stress, chemical exposure, and thermal swings. Many facilities default to standard carbon steel or basic coatings, only to face premature wear, pitting, or cracking within a few operating cycles. Instead, options such as duplex stainless steels, high-performance alloys, and advanced ceramics often prove their worth by resisting corrosion fatigue and maintaining dimensional stability long after conventional materials have degraded.
The key is matching the material’s microstructure to the specific failure modes of the application. For example, where abrasive slurries cause erosion-corrosion, a hardfaced or cladded surface can dramatically extend service intervals. In high-temperature cyclic operations, materials with low thermal expansion and good creep resistance—like certain nickel-based superalloys—prevent distortion and stress cracking. This targeted approach avoids the trap of over-specifying expensive materials where they aren’t needed while ensuring no weak link compromises the entire system.
Longevity also comes from thinking about how materials behave at interfaces and joints. Galvanic corrosion at dissimilar metal connections, fatigue at weld toes, and localized attack under deposits are common culprits in shortened asset life. By choosing compatible materials, using proper filler metals, and designing out crevices, operators can break the cycle of repeated repairs and replacements. In the end, the materials that outlast harsh industrial cycles are rarely the cheapest upfront—but they often deliver the lowest total cost per operating hour.
Precision Machining Details Behind Leak-Free Metal Seals
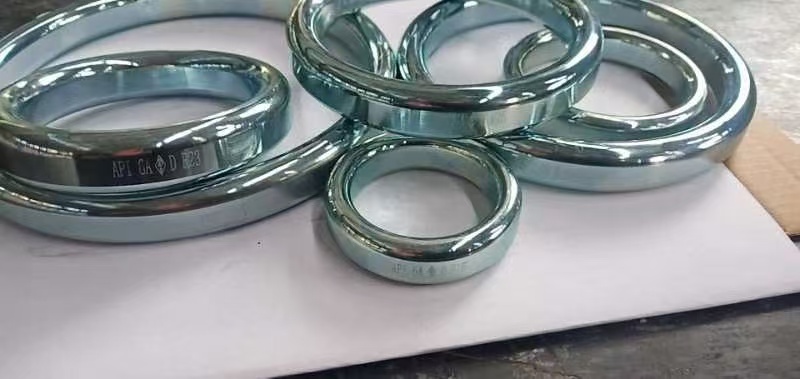
Achieving a leak-free metal seal starts with tolerances that most machine shops never need to hit. The mating surfaces are finished to a flatness and roundness within a few tenths of a micron, often using jig grinders or ultra-precision lathes. Surface roughness stays below Ra 0.05 µm, which leaves no continuous valley for pressurized fluid to creep through. Every ring gets checked with a laser interferometer, not just sampled, because a single shallow wave or taper on the face is enough to open a leak path under load.
Machining sequence matters as much as the final cut. Polycrystalline diamond tooling takes the last pass to avoid work hardening or micro-cracking that could later propagate. Coolant temperature is regulated to within half a degree Celsius because even a slight thermal drift during finishing will knock the part out of spec. After the final operation, some manufacturers run a deep cryogenic cycle to relax residual stress, reducing the chance that the sealing face distorts after installation.
Custom Ring Joint Profiles for High-Pressure and Corrosive Media
Standard ring joint gaskets fall short when sealing systems encounter aggressive chemicals, extreme thermal cycling, or pressures beyond typical API 6A ratings. Custom profiles address these gaps by altering the cross-sectional geometry—think oval, octagonal, or modified delta shapes—to distribute bolt load more evenly across the flange face. For chloride-rich environments, a slightly convex sealing surface paired with a controlled hardness differential prevents galling while maintaining a tight metal-to-metal contact. Engineers often specify tighter corner radii or asymmetric angles to direct residual stress away from stress-corrosion cracking zones, which extends gasket life in sour service.
Material selection works hand in hand with profile geometry. Nickel-based alloys like Inconel 625 or Hastelloy C-276 are common, but the real advantage comes from tailoring the ring’s cross-section to the flange’s deflection behavior under load. A deeper groove engagement with a shallower apex angle reduces the risk of unloading during pressure spikes, while a slightly wider base improves stability in vibrating piping systems. Some custom designs incorporate a two-stage sealing lip: the primary lip deforms plastically on initial bolt-up, and a secondary elastic lip compensates for thermal expansion differences between the flange and the gasket.
Field feedback shows that custom ring joints are not just for exotic applications. In refineries handling high-temperature hydrogen streams, a modified octagonal profile with a tapered inner edge has cut leak rates by over 40% compared to standard rings, simply because it matches the actual flange groove machining tolerances. The key is to avoid copying catalog dimensions; instead, map the flange’s surface finish, bolt spacing, and expected pressure-temperature envelope, then let the profile follow that data. For critical joints, prototype testing under simulated cycling conditions is worth the lead time—a ring that survives 500 thermal shocks in the lab will outperform a generic shape every time.
Fast Delivery of Exotic Alloy Gaskets Without Compromising Quality
Getting hold of specialty alloy gaskets usually means waiting weeks, but our streamlined stock program turns that on its head. We keep a deep inventory of hard-to-find materials like Hastelloy, Inconel, Monel, and titanium in common and custom sizes. When you place an order, it ships within 48 hours from one of our regional hubs—no expediting fees, no frantic phone calls. The secret is a lean manufacturing setup that cuts out batch-processing delays while keeping every piece traceable to its heat lot.
Speed doesn't mean skipping the details. Every gasket that leaves our dock has passed a multi-point inspection: dimensional checks against ASME B16.20, hardness testing on the metal core, and a full visual scan for surface defects. We also run random lot samples through compression-recovery tests to verify sealing performance under real flange loads. If a gasket doesn't meet our internal tolerance bands—tighter than industry norms—it gets scrapped, not shipped. That's how we can promise a 48-hour turnaround without a single compromise on material integrity or seal reliability.
What really sets us apart is the way we handle rush jobs. Instead of pushing a standard order aside, we pull from a dedicated emergency stock reserved for breakdowns and turnarounds. You get the same exotic alloy, the same full documentation package, and the same quality sign-offs, just on a compressed timeline. No one else in this space pairs that kind of speed with genuine metallurgical verification—because we built our whole process around doing both at once.
Surface Finish Secrets That Improve Gasket Performance
Most gasket failures blamed on material or torque trace back to the mating surface. The numbers on a profilometer trace don't tell the whole story, but they do point to how a gasket will bite into the flange. A surface that's too polished leaves the gasket nothing to key into, which can encourage lateral creep and eventual extrusion under thermal cycling. Too rough, and the peaks hold the gasket away from the valleys, leaving tiny leak paths that only open once system pressure climbs.
Lay direction is the overlooked variable. Machining marks that run straight across the sealing face behave differently than a phonographic spiral. If the lay runs parallel to the pressure boundary, you can get a continuous channel from inside to outside. A controlled spiral or cross-hatch interrupts that path and gives the gasket a more uniform seating surface. Waviness matters just as much as roughness; a surface can show a perfect Ra number yet have a wave height that fluctuates enough to create low-load zones where the gasket never reaches design compression.
Instead of chasing a single roughness value, look at the full profile. After machining, run a quick visual check for chatter marks, deep scoring, and uneven tool paths. A light deburr can knock down sharp peaks without polishing away the texture that helps the gasket grip. If repeated scallops show up or the face feels too slick, the surface isn't ready for a gasket that has to survive pressure spikes and thermal swings.
On-Site Support and Failure Analysis for Unplanned Shutdown Prevention
When production lines grind to a halt without warning, the cost rarely stops at lost output. Our field engineers arrive with toolkits and structured diagnostic protocols that treat every shutdown as a chain of measurable events rather than an isolated component failure. They check vibration signatures, thermal cycling records, and lubrication residue on-site, turning scattered symptoms into a coherent failure timeline.
Failure analysis goes beyond the obvious broken part. We collect fracture surfaces, oil samples, and control logs before they are disturbed, then run metallurgical and signal reviews back at the lab. This often uncovers hidden triggers such as voltage sags, contaminated batches, or repeated micro-overloads that standard maintenance checklists miss.
The real payoff is prevention. By matching on-site findings with asset history, we produce a short, prioritized list of corrective actions—torque recalibration, cooling circuit flushing, or drive parameter tuning—that operators can implement during the next planned window. The goal is not just to restart the line, but to make the next unplanned stop far less likely.
FAQ
Their octagonal or oval cross-section bites into the flange faces as bolts are tightened, creating a metal-to-metal seal that holds up under extreme pressure and temperature swings. That mechanical grip is what keeps pipelines and wellheads from leaking when softer gaskets would simply blow out.
Look for a supplier who asks about your operating pressure, temperature range, and fluid compatibility before recommending anything. A reliable partner will provide material traceability, hardness test reports, and dimensional checks rather than just shipping generic parts from a catalog.
Soft iron is the default for standard oil and gas service because it deforms enough to seat properly without damaging flanges. For sour service or corrosive chemicals, you need something like 316 stainless, duplex, or Inconel—using the wrong alloy leads to premature corrosion or flange galling.
The gasket has to embed into the flange groove, so a rough or damaged finish prevents a full metal-to-metal contact. Even a small nick or rust pit can create a leak path, which is why careful surface prep and inspection are just as important as torque values.
Visible corrosion, pitting, or scoring on the sealing surface is an obvious red flag. Also watch for uneven compression marks after disassembly, or if the gasket hardness has increased significantly from repeated thermal cycling—it loses the ductility needed to reseal.
Generally no. Once a ring joint gasket has been compressed, it work-hardens and loses the ability to conform to the flange groove again. Reusing one might save a few dollars upfront, but it frequently results in leaks and expensive unplanned downtime.
These standards define dimensions, tolerances, material hardness limits, and marking requirements. Buying gaskets that meet them ensures the part will fit standard flanges and perform as expected—anything that skips these certifications is a gamble for critical service.
They should recommend alloys based on actual fluid chemistry, not just general categories. The supplier should also check that gasket hardness stays below the flange hardness to protect the groove, and often they'll provide passivation or coating options to extend service life in aggressive media.
Conclusion
When a sealing failure can halt an entire operation, the choice of ring joint gasket supplier becomes a matter of uptime and safety rather than just procurement. This supplier focuses on material grades that hold up under extreme thermal cycling and aggressive process fluids, pairing them with precision machining tolerances that eliminate the micro-leak paths common in lower-quality seals. Instead of offering only standard sizes, the team works from detailed pressure and corrosion data to produce custom ring joint profiles, including oval and octagonal cross-sections in duplex, super duplex, Inconel, and other exotic alloys. Rapid turnaround on these specialized orders does not mean cutting corners; each batch passes dimensional checks and hardness verification before it leaves the shop.
Surface finish is treated as a functional parameter, not a cosmetic afterthought, with controlled roughness values selected to match the flange condition and service environment. For sites facing recurring gasket blowouts or unexplained emissions, the supplier provides on-site inspection and failure analysis, tracing root causes such as flange rotation, incorrect bolt loading, or surface damage. This diagnostic approach helps prevent unplanned shutdowns before they occur, turning gasket supply into a reliability partnership. The result is a sealing solution that handles high-pressure, high-temperature, and corrosive media without compromising leak-tightness or delivery timelines.
Contact Us
Contact Person: Kaxite
Email: [email protected]
Tel/WhatsApp: 0086-574-87527771
Website: https://www.seal-china.com