Boron Carbide Manufacturer: A Buyer’s Guide to Quality, Consistency, and Technical Support
2026-10-19
Sourcing boron carbide that actually delivers on its specs isn't a given — too many suppliers cut corners on purity, particle size, or batch-to-batch consistency. Before you commit to a purchase order, you need more than a data sheet; you need a manufacturer that treats technical support as part of the product. HUAYI TECH has built its reputation on that exact pairing of rigorous quality control and real engineering collaboration. In this guide, we break down what separates a dependable supplier from a costly gamble — and why those differences matter for your armor, abrasive, or nuclear application.
When a Boron Carbide Spec Sheet Is Not Enough
A boron carbide spec sheet usually lists density, hardness, flexural strength, and maybe fracture toughness. Those numbers are useful for a first screening, but they rarely predict what happens when a projectile hits at an odd angle or when the plate is backed by a soft armor pack that deforms differently than the test fixture. I've seen plates pass every line item on paper yet crack prematurely in field trials because the spec didn't account for multi-hit spacing or thermal shock from a rapid temperature swing.
Another gap is the microstructure. Two batches can have identical density and hardness but very different grain size distributions, porosity clusters, or sintering defects. A spec sheet won't tell you if the boron carbide has uneven carbon content near the surface, or if the hot pressing left residual stresses that only show up under high strain rate loading. Without metallographic data, you're essentially buying a black box that meets a few nominal values.
The practical fix is to build your own acceptance protocol around realistic testing. That might include ballistic tests with the actual threat and backing, ultrasonic scanning for internal flaws, and periodic sectioning to check grain structure. Some teams also track lot-to-lot variation with statistical control charts instead of relying on a single certificate of conformance. In critical applications, the extra effort costs far less than a field failure.
Why Some Boron Carbide Batches Fail in the Field
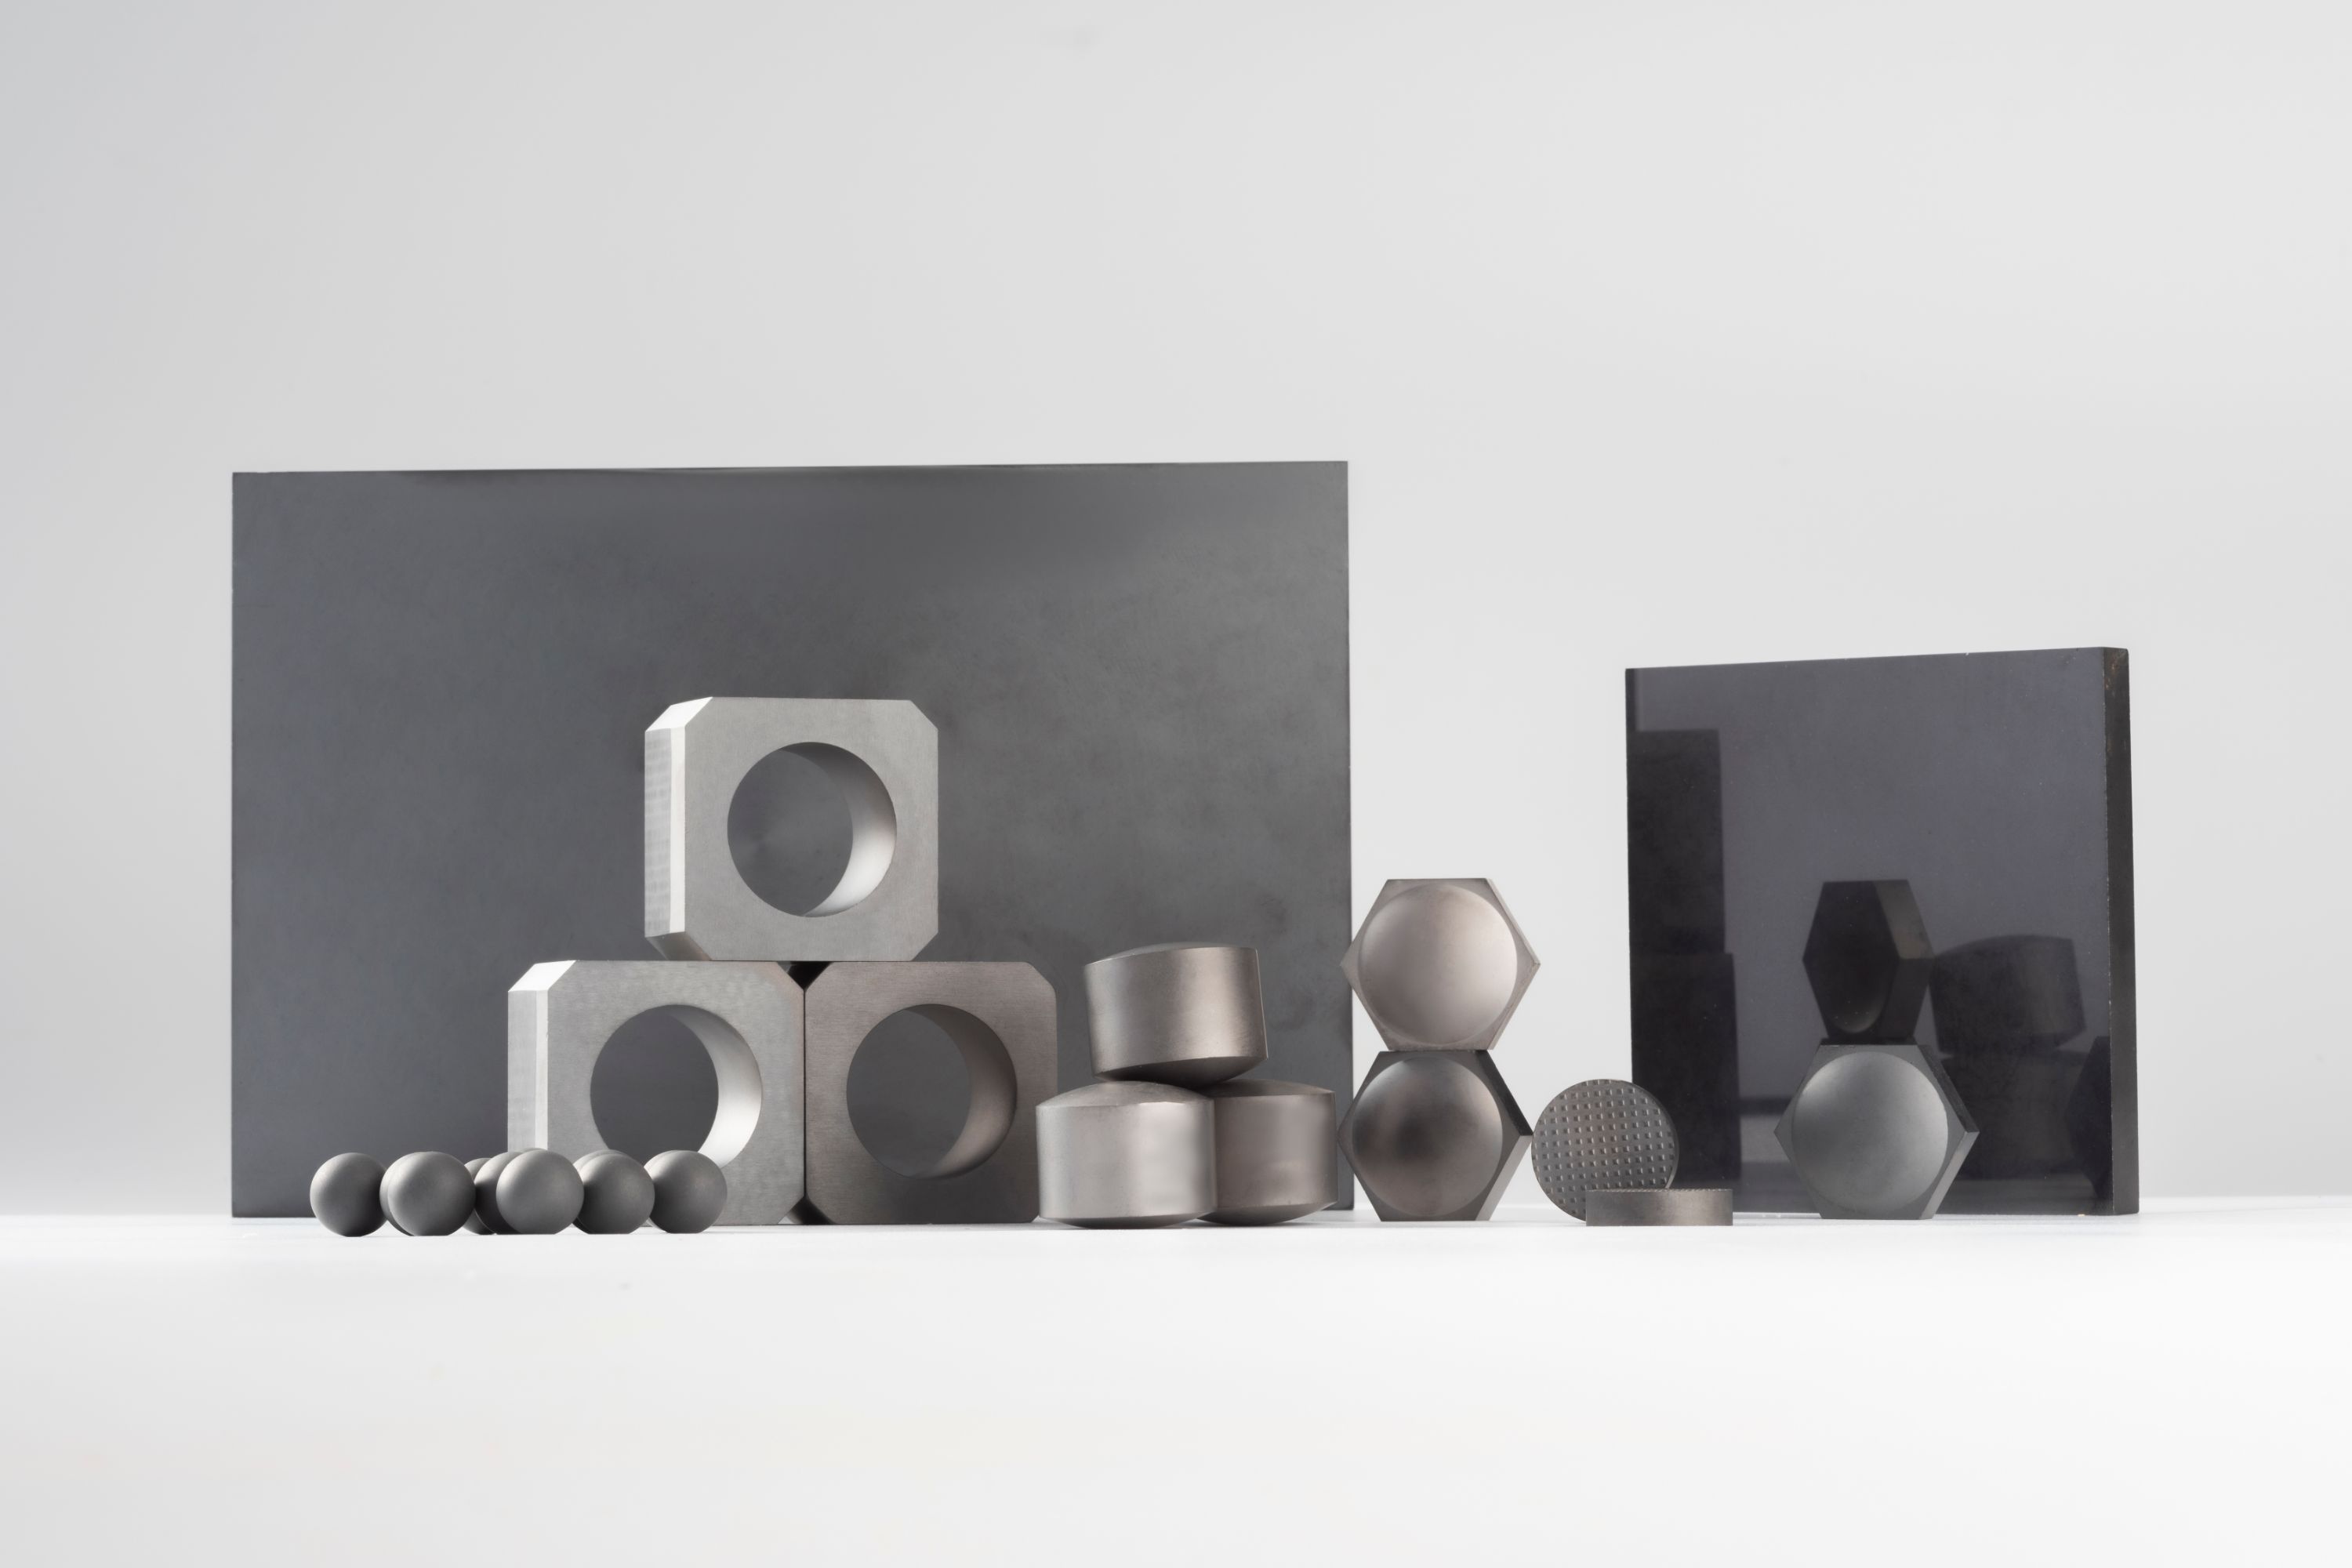
Boron carbide fails in service for reasons that are usually decided long before the batch leaves the plant. Small shifts in the boron-to-carbon ratio, free carbon clusters, or oxygen pickup from raw powders can leave the finished ceramic with lower hardness and a much higher sensitivity to crack initiation. A plate that passes a simple density check can still carry these defects, and they only show up when the material faces a high-strain-rate impact.
Sintering irregularities are another common culprit. Hot-pressed boron carbide can develop density gradients if the die temperature is uneven, or if the pressure ramp is too fast. Those gradients create residual stress, which encourages microcracking along grain boundaries. Over time, or under repeated hits, those microcracks link up and the component loses multi-hit capability even though the quoted areal density looks fine on paper.
Finally, trace impurities from grinding media or furnace linings sometimes get incorporated into the batch. Metallic inclusions act as stress concentrators, while boron oxide films weaken bonding between grains. Field failure is therefore rarely a single dramatic event: it is the outcome of several small processing compromises that were invisible in routine acceptance tests but become critical under real loading.
Getting Technical Help Before You Need It
One of the least glamorous but most valuable moves you can make on any technical project is to line up your help channels before you actually need them. This means knowing who to ping when a build breaks, where to file a ticket for a permissions issue, and which docs actually cover the edge cases you're likely to hit. It's not about being paranoid—it's about saving yourself from the 2 a.m. scramble when something goes sideways.
For example, if you're spinning up a new service or working with an unfamiliar API, take fifteen minutes to skim the internal wiki or ask a teammate which support alias responds fastest. That tiny bit of groundwork can turn a potential day-long blocker into a five-minute fix. You'll also start to notice patterns: maybe the database team prefers Slack over email, or the infra folks need a specific log snippet before they'll even look at your issue.
Building a rapport with the people who provide technical help pays off in ways that don't show up in a ticket queue. When you reach out early, share context, and show you've done some initial digging, you're more likely to get a thoughtful response instead of a canned one. And if a real crisis does hit, you'll already know the right door to knock on.
Impurities That Quietly Sabotage Your Process
Trace metals, moisture, and organic residues rarely announce themselves. A few parts per million of iron in a catalyst bed can shift selectivity by 30 percent before anyone notices the yield drift. The worst part is that these contaminants often mimic normal variability, so teams spend weeks tuning temperature or pressure while the real culprit sits in a raw material drum.
In polymer extrusion or solvent-based coating, low-level peroxides and aldehydes can cross-link or gel at exactly the wrong moment. A single contaminated lot of monomer can turn a stable recipe into a batch-to-batch lottery. Instead of blaming the operator or the weather, the fastest diagnostic is often a simple lot-to-lot impurity profile.
Even "inert" surfaces contribute. Leached plasticizers from tubing, rust from a storage tank, or silicone oil from a seal can accumulate in recirculating systems. These impurities don't just reduce purity; they change viscosity, wetting, and adhesion in ways that are hard to reverse downstream. Building a short list of likely contaminants for each feed stream turns an invisible saboteur into a manageable variable.
Supplier Audits Without the Smoke and Mirrors
Most supplier audits fail before they start. The standard drill—scheduling visits weeks in advance, asking for the same policy binders, ticking compliance boxes—gives a factory plenty of time to stage a Potemkin village. Workers get coached, records get polished, and the real problems stay hidden behind fresh paint and rehearsed answers. If you want to see what actually happens on a Tuesday night, show up unannounced. Walk the floor without the guided tour. Check the lockout/tagout log against machine maintenance dates. Ask a line operator, not the plant manager, when the last safety incident occurred. The truth is usually in the gaps between what's documented and what's done.
That means ditching the checklist mentality. A checklist tells you whether a supplier can produce paperwork. It rarely tells you whether they can produce your product without cutting corners. Instead of auditing against a generic ISO template, build the audit around your own failure modes. If late deliveries have been creeping up, trace the raw material receiving dates and compare them to promised lead times. If quality complaints cluster around a specific shift, sit in on that shift's handover meeting. Look for informal workarounds—pallets of rejected parts tucked behind a warehouse, handwritten notes overriding the ERP system, calibration stickers that are suspiciously fresh. These are the real indicators of a supplier's operating culture.
Finally, make the audit a conversation, not an interrogation. Suppliers hide problems because they expect punishment. If every finding turns into a lecture or a penalty, you're training them to lie better. Instead, share your own factory's near misses and ask what they'd do differently. Offer to jointly fix a labeling issue rather than just scoring it. When a supplier trusts that transparency leads to support rather than retribution, the smoke clears. You'll start hearing about the machine that's been limping along for months, or the sub-tier vendor who's been shipping borderline material. That's the kind of information no scheduled audit or polished presentation will ever reveal.
Long-Term Supply Without Quality Surprises
Sustaining a dependable supply stream over months and years demands more than locking in a vendor. We treat each production batch as part of a longer conversation with the factory floor, tracking subtle shifts in raw material sourcing, line speed, and outgoing inspection data before they become visible defects. When a parameter drifts—even one that still falls inside a formal tolerance—our teams adjust the process now, not after customers notice.
That forward-looking stance removes the usual cycle of rushed rework and emergency air freight. It also lets buyers plan their own inventory with confidence, because the part arriving in month twelve behaves like the sample approved in month one. The result is a supply arrangement where quality is not a periodic surprise, but a steady background condition.
FAQ
Start with their production method and raw material traceability. A manufacturer that controls the powder synthesis and sintering in-house can usually demonstrate tighter batch-to-batch control than one that outsources these steps.
Ask for a full certificate of analysis that includes not just total boron and carbon, but also free carbon, oxygen, nitrogen, and particle size distribution. Then request a sample from the new lot and run your own density and hardness checks before committing to a large order.
You should be able to reach a materials engineer who understands your specific application, whether it's ballistic armor, abrasive blasting, or nuclear shielding. They should help with pressing parameters, sintering profiles, and troubleshooting rather than just reading a datasheet back to you.
Yes, and it shows up in final density and fracture toughness. Hot-pressed parts often reach higher density with less sintering aid, which matters for armor performance. Pressureless sintering can be more cost-effective for complex shapes, but you need to confirm the density and porosity limits for your design.
Request third-party inspection before shipment, and do not rely on the supplier's own lab. Pay attention to packaging consistency and moisture protection. Also order a small trial batch under the exact same shipping conditions before scaling up.
Ask for historical SPC data on density, hardness, and particle size across at least five consecutive lots. Clarify what happens if a lot falls outside the agreed specification: will they replace it, discount it, or ask you to accept it? A supplier with a documented nonconformance process is far safer.
If your component has tight tolerances, requires a custom sintering profile, or will be used in a safety-critical application, the extra support pays for itself quickly. Otherwise, you risk spending more on machining scrap and field failures than you saved on the powder price.
Conclusion
Spec sheets rarely tell the whole story with boron carbide. A data sheet can list 98% purity and a tight particle size range, yet those numbers won't predict how a batch behaves under your specific pressing or sintering conditions. Over the years, I've seen buyers accept a certificate of analysis at face value only to watch parts crack, wear unevenly, or fail ballistics tests. That's the gap where technical support should step in before problems surface—not as a rescue call after a rejected lot. The most reliable suppliers pair each shipment with metallurgical context: how the powder was milled, what oxygen pickup occurred, and whether the boron-to-carbon ratio shifted during processing. Impurities like free carbon, silica, or iron oxide often sit just below detection limits on standard reports, yet they can quietly alter densification or reduce hardness in the final component.
A buyer's real leverage comes from audits that look past polished presentations and sample kits. Ask to walk the production floor, not just the conference room. Watch how raw materials are quarantined, how blending records are kept, and whether the lab runs cross-checks against an independent referee. Consistency over a two-year contract matters more than a single perfect batch. Look for a supplier who tracks lot-to-lot variation using process control charts and isn't afraid to share those trends with you. Long-term supply without quality surprises means the manufacturer treats every order as part of a continuing production run, not a one-off transaction. When that mindset is paired with early technical dialogue, you end up with a boron carbide source that supports your process rather than just filling a purchase order.
Contact Us
Contact Person: Junting Leo
Email: [email protected]
Tel/WhatsApp: +86 18615009766
Website: https://www.huayimaterial-china.com/