OEM Press Brake Machine Key Factors to Consider Before Buying
2026-09-15
Choosing the right OEM press brake machine can feel overwhelming, especially with so many technical specs and performance claims competing for your attention. Before you commit to a purchase, it’s crucial to cut through the noise and focus on the factors that truly impact productivity, accuracy, and long-term value. At HUNSONE, we understand that every bending application is unique—and we’re here to help you make an informed decision. In this guide, we’ll walk through the key considerations that separate a reliable workhorse from a costly mistake.
Why Tonnage Numbers Alone Mislead Buyers
A 3-ton air conditioner sounds bigger and better than a 2-ton, but that number only tells how much heat the unit can move under ideal lab conditions. It doesn’t account for your home’s layout, window placement, duct leakage, or how well the envelope is sealed. So two houses with identical 3-ton systems can end up with very different comfort and energy bills.
Many buyers get pushed toward higher tonnage because it feels like more cooling power, but an oversized unit cycles on and off too quickly. It never runs long enough to pull humidity out of the air, leaving the space clammy and musty. Meanwhile, a properly sized smaller unit often delivers steadier, drier comfort and lower long-term costs.
Instead of judging by tons alone, pay attention to a room-by-room load calculation and the installer’s track record. Real-world performance comes from matching the system to the house, not from a bigger number on a label.
The Frame Flex Test Most Spec Sheets Skip
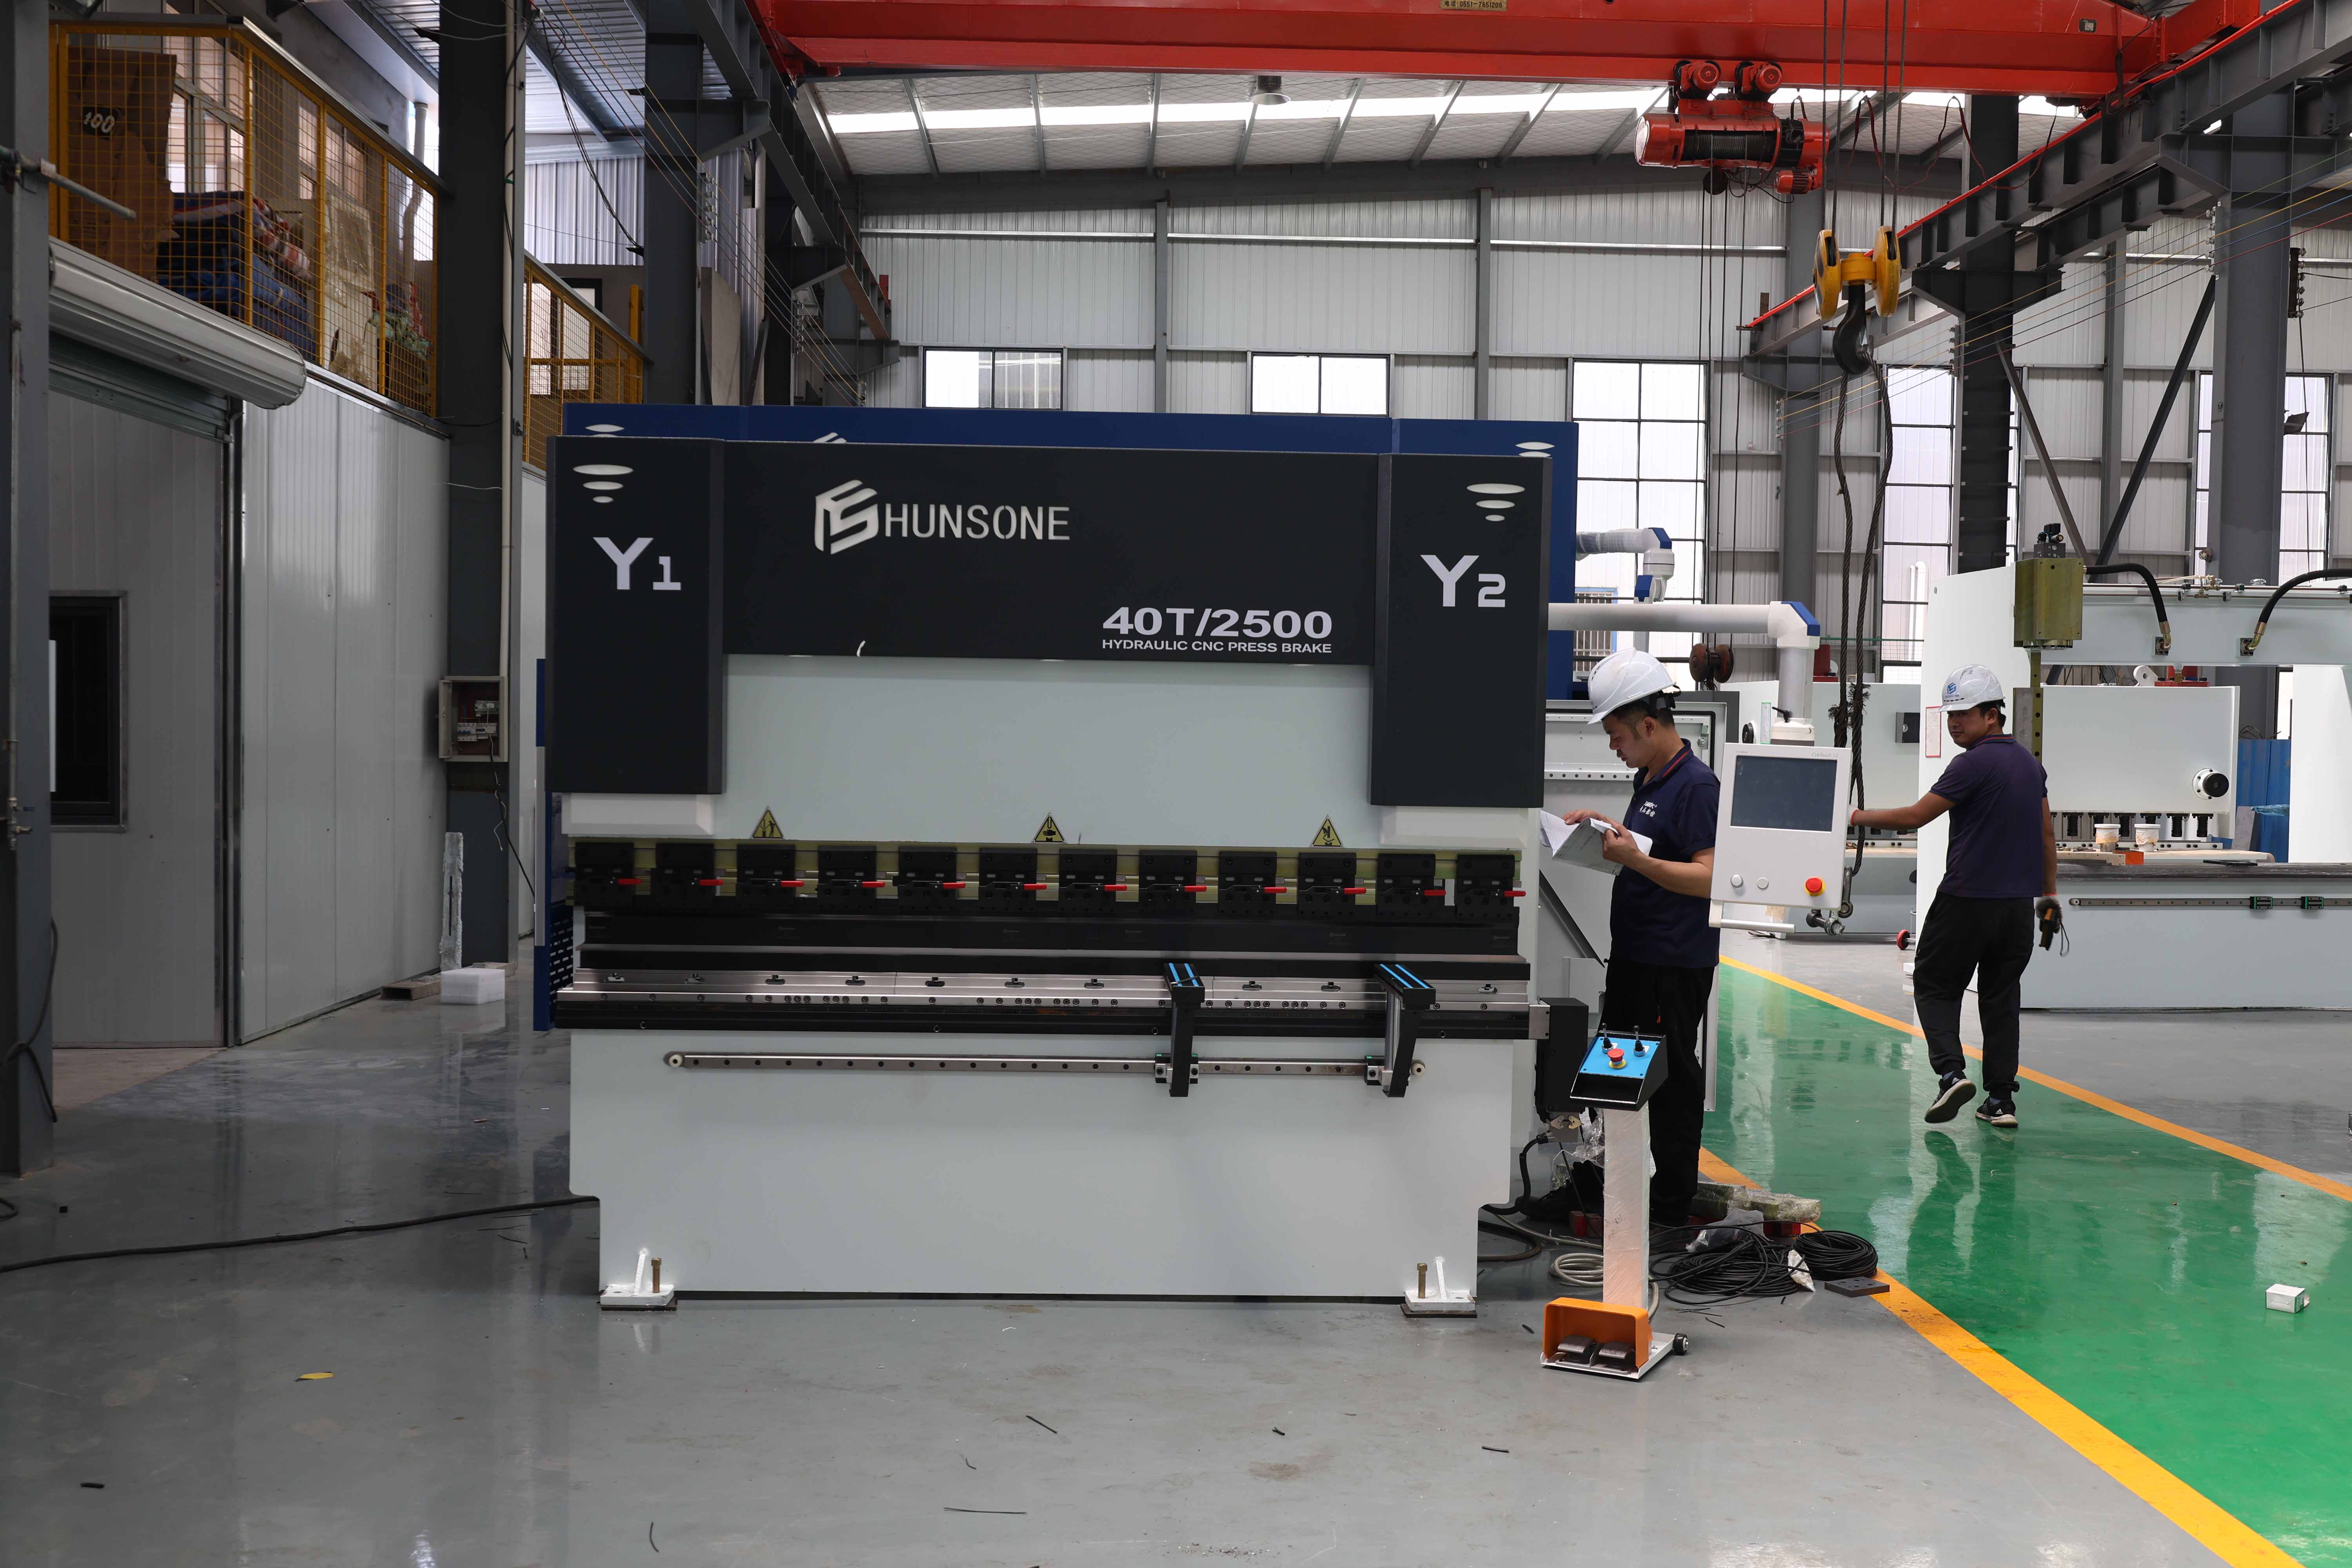
Most spec sheets will list weight, geometry, and maybe tire clearance, but they rarely show how a frame behaves under load. The frame flex test that gets skipped involves anchoring the bottom bracket and measuring lateral deflection at the head tube while applying a controlled side load. It is not about making a frame noodle-soft or rock-hard; it is about mapping where the flex happens and whether it returns energy in a predictable way. A bike that twists too much at the bottom bracket can feel vague when you stomp on the pedals, while one that is overly rigid in the rear triangle may chatter through rough corners instead of holding a line.
To run a meaningful version of this test, you need a repeatable setup: clamp the frame at the dropouts, hang a known weight from the bottom bracket shell, and measure deflection with a dial indicator. Then repeat the load from the opposite side to check for asymmetry. The numbers you get are rarely printed anywhere, but they tell you more about sprint response and high-speed stability than a 50-gram weight difference ever will. Riders who pay attention to this kind of deflection data often find they prefer a frame with slightly more lateral give in the top tube and a stiffer down tube, because it filters road buzz without sacrificing steering precision.
Backgauge Consistency Over a Thousand Bends
Over a thousand bends, a backgauge that drifts even 0.05 mm per cycle will produce a cumulative error large enough to scrap a high-precision part. The problem rarely shows up in a single stroke. It appears as a slow thermal expansion of the gauge bar, slight loosening of a coupling, or micro-slip in a belt drive after continuous cycling. Operators often notice it as an unexpected change in flange length halfway through a batch, with no obvious cause. The only way to catch it before it ruins work is to treat backgauge repeatability as a dynamic characteristic, not a static spec.
Consistent positioning depends more on the mechanics of the gauge's drive train than on the controller's resolution. A rigid, one-piece gauge bar mounted on preloaded linear guides resists the torsional flex that shows up when the gauge moves off-center. Zero-backlash ballscrews or direct-drive linear motors remove the lost motion that accumulates in cheaper belt or rack systems. Closed-loop feedback at the point of measurement—where the gauge finger actually touches the sheet—corrects for belt stretch and thermal growth, rather than assuming the motor's encoder reflects reality. Regular re-referencing against a fixed stop after every few hundred cycles also resets any micro-drift before it compounds.
A thousand-bend validation run tells you more than any spec sheet. Run a standard 2 mm mild steel blank with a 90° bend, measure the backgauge stop position every 10 bends, and record the flange length from a sample every 50 bends. On a well-built press brake, the total spread across the entire run should stay under 0.03 mm, with no gradual trend upward or downward. If you see a sawtooth pattern or a slow climb, something in the gauge assembly is wearing or heating unevenly. That kind of data, gathered over hours of continuous cycling, separates a backgauge that is merely accurate at startup from one that stays consistent until the job is done.
Controls That Slow Down or Speed Up Setup
Every production environment has hidden levers that determine how quickly a new machine or process can go from zero to full operation. Some of these controls are obvious, like a well-designed quick-release clamping system that drops changeover time from twenty minutes to under five. Others are less visible: the placement of calibration dials, the length of cable runs, or even the type of thread used on adjustment screws. What often separates a painfully slow setup from a fast one is not the number of steps, but whether each step requires a separate tool, a specific torque value, or a trained eye to verify.
On the slowing side, you find controls that demand excessive precision without offering feedback. A depth stop that must be set with a feeler gauge and then re-checked after every batch will eat hours over a week. Similarly, software interfaces that bury a critical offset parameter three menus deep create a hidden tax on operators who just need to tweak one value. These slowdowns rarely show up in a specification sheet; they reveal themselves only after the third or fourth time you watch someone struggle through the same setup sequence.
By contrast, controls that speed things up share a common trait: they reduce the need for judgment calls. A spring-loaded detent that clicks into the correct position, a color-coded hose that can only be attached one way, or a digital readout that shows the exact offset without requiring a calculator — each removes a small hesitation. The cumulative effect is dramatic. When setup stops being a puzzle and starts being a rhythm, throughput climbs, errors drop, and the person doing the work stops dreading the next changeover.
Spare Parts Realities After the OEM Handoff
The moment a production line stops stamping out a given model, the parts ecosystem shifts quietly but irreversibly. OEM vendors often sell remaining stock to liquidators or authorized aftermarket distributors, and from that point onward, availability becomes a game of leftovers and lottery tickets. A water pump for a seven-year-old sedan might sit on a dusty shelf in Ohio one week and vanish the next, leaving repair shops scrambling across regional warehouses and online marketplaces where “new old stock” can mean factory sealed or simply repackaged returns.
Quality control after the handoff is where the real friction shows up. Third-party manufacturers reverse-engineer high-demand components, but tolerances drift, material grades get swapped, and coating specs quietly disappear. A replacement control arm might bolt in perfectly yet fail after 15,000 miles because the bushing compound was downgraded from natural rubber to a cheaper synthetic blend. Independent repairers learn to keep a mental blacklist of part numbers that look identical on a screen but behave differently once torqued under load.
Pricing stops following the old logic too. Scarcity drives spikes that have nothing to do with manufacturing cost — a discontinued HVAC blend door actuator can jump from $40 to $300 in a single season. Meanwhile, some “OEM surplus” listings are actually counterfeit boxes with convincing holograms, and spotting the difference often requires comparing laser etching depth or connector pin plating under magnification. The handoff doesn’t just change where parts come from; it rewrites who you can trust and how much verification each purchase demands.
Hidden Power Draw When the Ram Is Idle
Most people assume a memory stick that isn't being actively read or written draws almost no power, but that's far from true. Even when the system is idle, DRAM cells have to be refreshed thousands of times per second just to keep their charge from leaking away. That refresh cycle runs constantly and pulls a small but steady current from the power supply. On top of that, the memory controller on the CPU side stays clocked and ready, and the data bus termination resistors remain active, so a measurable power draw continues in the background.
The exact idle consumption depends on the type and configuration of the RAM. Older DDR3 modules, for instance, often idle at a lower voltage than DDR4 or DDR5, but high-density kits with aggressive XMP profiles can push idle power up noticeably because the memory is kept at a higher voltage and tighter secondary timings. Registered or buffered DIMMs used in servers draw even more at idle due to the register chips and extra termination circuits. It's not a huge amount per stick, but in a multi-DIMM setup or a system running 24/7, the hidden drain adds up.
One way to reduce this idle power is to let the memory enter a deeper low-power state, such as self-refresh, when the system isn't busy. Some BIOS settings allow you to enable aggressive power-down modes or lower the memory voltage manually, though that may affect stability. Another practical step is to avoid populating every memory slot if you don't need the extra capacity, since each additional stick adds its own idle current. Keeping an eye on this often-overlooked drain can make a real difference in total system power consumption.
FAQ
The frame is the backbone, so look for full penetration welds and evidence of stress relieving. A machine that has not been stress relieved will gradually lose accuracy as internal stresses release during the first few years of hard use.
A control that requires three extra steps for a simple bend will frustrate even a skilled operator. Look for a system that stores tooling data, calculates bend allowance automatically, and lets you recall a job by part number rather than by re-entering every dimension.
Tonnage depends on the material type, the bend length, the V-die opening, and the required bend radius all at once. Using the standard rule of thumb without checking the actual required force can either damage the tooling or leave you with a machine that is too small for your typical jobs.
The backgauge positions the sheet for each bend, so its accuracy and stiffness matter as much as the ram's. A flimsy backgauge will flex when the sheet hits it, leading to inconsistent flange lengths, especially on thicker or heavier parts.
If you run a lot of short, fast bending cycles and want lower energy use, an electric drive often makes sense. But if you need high tonnage at slower speeds and already have maintenance experience with hydraulic systems, a hydraulic machine is still hard to beat for reliability in heavy plate work.
Check the clamping system and the tooling height standard before you buy. Some OEM machines use proprietary tool holders that lock you into one supplier's expensive consumables, while others accept common European or American style punches and dies, which keeps tooling costs and lead times under control.
People focus on the upfront price and forget about daily lubrication points, hydraulic oil filtration, and the availability of local service technicians. A machine that needs a technician flown in from another city for a simple sensor replacement will cost you far more over ten years than a slightly higher initial quote.
It should match your typical part size for efficiency, not your largest possible job. Buying a 12-foot machine when 90 percent of your work is under 4 feet means you pay for extra floor space, higher power consumption, and more crowning adjustment for every small part, without any real benefit on most days.
Conclusion
Many buyers fixate on the tonnage figure, but that number can mislead if you don't know how force drops off when the bend isn't centered. A machine rated at 100 tons may only deliver 70 tons near the frame ends once deflection sets in. Ask for the frame flex test data that most spec sheets leave out; that will tell you more about real capacity than the headline number. Then watch the backgauge for a thousand bends, not just a demo cycle. Thermal drift, ballscrew backlash, and repeatability errors start showing up after prolonged runs, and that's where consistency is won or lost. Setup speed also depends heavily on the control. Some interfaces bury a tooling change under six menu layers, while others let you import a bend program, adjust the angle correction, and hit run in seconds. The difference shows up every time you switch from a simple bracket to a multi-bend panel.
Once the OEM hands over the machine, spare parts become a daily reality. Ask which wear items are truly off-the-shelf and which are proprietary castings or custom manifolds with eight-week lead times. Some manufacturers keep regional stock; others ship from a single overseas warehouse. Idle power draw is another overlooked cost. The hydraulic pump, cooling fan, and control cabinet often keep consuming electricity even when the ram is not moving. Over a year of two-shift operation, that hidden draw can add thousands to your energy bill. So before signing, look beyond cycle time and maximum tonnage. Evaluate how the frame behaves under off-center load, how repeatable the backgauge stays after hundreds of parts, how fast the control gets you from first part to approved part, and what happens when a servo valve fails on a Tuesday morning.
Contact Us
Contact Person: James Chen
Email: [email protected]
Tel/WhatsApp: 86 13770803946
Website: https://www.hunsone.com/